5 Gallon Water Bottle Line: Machine Configuration
TDB-25APC configuration for 3–5 gallon PC water bottles: specifications, material drying, mold and auxiliaries, with a downloadable datasheet.
ExploreManufacture better extrusion blow moulding machines for you.
Application engineering guide
How 3–5 gallon PC water bottles are made, the dedicated machine, and what to specify for material drying, mold, trimming and quality checks.
3–5 gallon PC water bottles are made by extrusion blow molding on a dedicated machine. Polycarbonate is dried, then plasticized under controlled temperature and extruded as a parison; the mold closes and compressed air forms the bottle with its neck and handle. After cooling, the bottle is trimmed and checked.
| Item | TDB-25APC |
|---|---|
| Products | 3–5 gallon water bottles |
| Materials | PC; Tritan configurations available in the product range |
| Stations | Single |
| Stated maximum product volume | 25 L |
| Clamping force | 215 kN |
| Plasticizing | Hydraulic-motor plasticizing arrangement |
Machine details: TDB-25APC · 10 process checks for 5 gallon PC bottles · Quotations: Tongda 5 gallon bottle machines (tongdamachine.net)
Making PC water bottles involves the material, extrusion system, mold, blow pin, cooling, trimming and downstream handling. Begin with a drawing or sample and define the nominal volume, dimensions, target weight, neck, handle and intended use. Those details provide a better basis for machine selection than the volume alone.
The PC bottle application uses a dedicated plasticizing and die-head arrangement. Specify the PC grade and drying requirements with the material supplier, and confirm the intended finished-bottle application. Drying, moisture control and controlled heating are important parts of the production plan.
The extrusion system melts the material and forms a hollow parison. The mold closes around the parison, air forms it against the mold cavity, and the part cools before removal. The neck and flash are finished according to the tooling arrangement. The material, parison program, mold and cooling must be tuned together during a production trial.
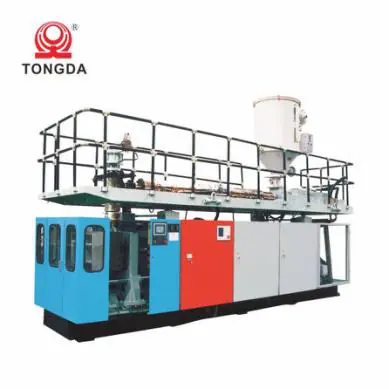
The TDB-25APC is the dedicated water-bottle model in the machine range. Review the resin grade, neck, handle, product weight and mold dimensions with the team. Different published application sheets can represent different configurations, so use the current project drawing for installation planning.
| Model | Stations | Stated maximum volume | Clamping force |
|---|---|---|---|
| TDB-25APC | Single | 25 L | 215 kN |
Agree output in accepted containers per hour for a named bottle, resin, weight and cavity arrangement. A dry-cycle rate does not include the complete production process. Cooling, extrusion, wall thickness, trimming and downstream handling affect finished-product output. Use an agreed trial to establish the result for the project.

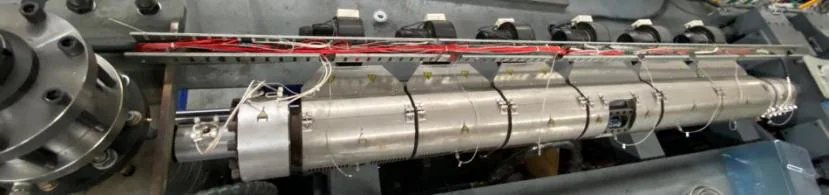
The PC bottle configuration uses a hydraulic-motor plasticizing arrangement for the PC bottle machine. Screw design, material preparation and temperature control work together to provide a consistent melt. Review the plasticizing configuration for the selected resin, with attention to cleanliness and material residence conditions.
The die head forms the parison from the plasticized material. Its flow path and tooling need to suit the material, product geometry and head arrangement. A parison-control system varies wall distribution along the parison. Evaluate the finished bottle sections, weight and required performance when setting the program during commissioning.
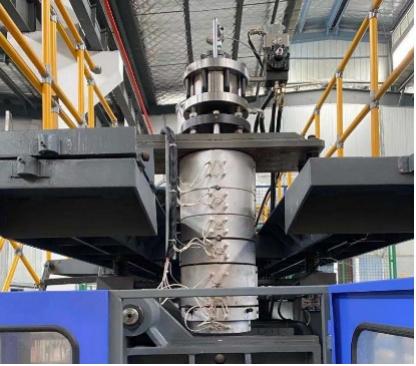
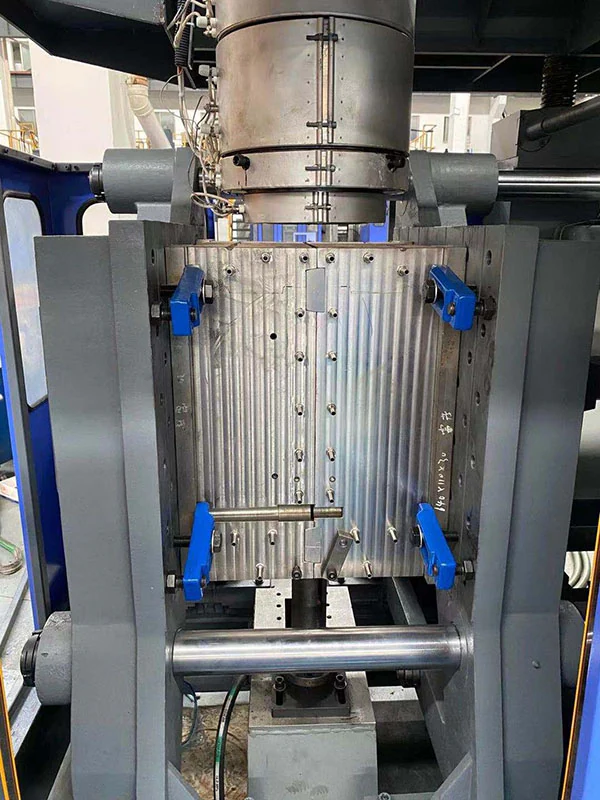
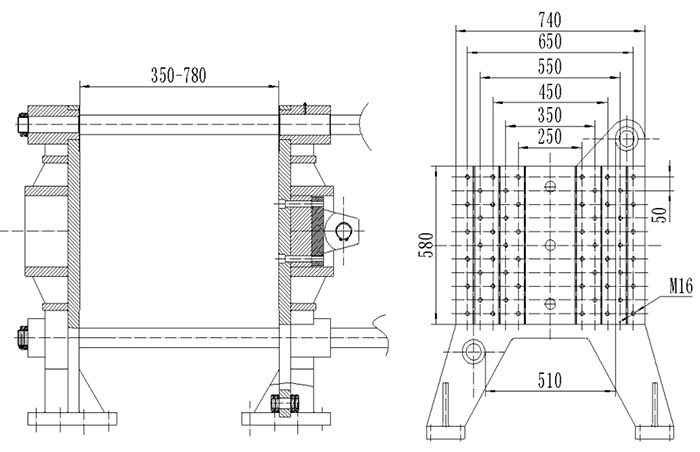
Review the mold’s external dimensions, required opening and mounting arrangement with the machine specification. The machine range shows guided mold movement, toggle clamping and different blow-pin arrangements. Select clamping force and mold support around the actual part and tooling; a larger force alone is not a substitute for a suitable mold design.
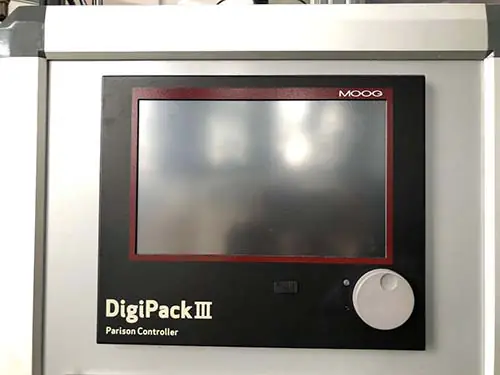
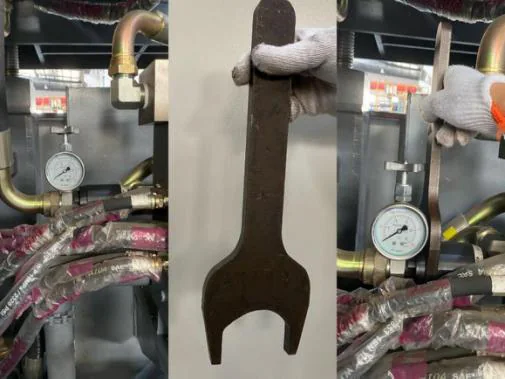
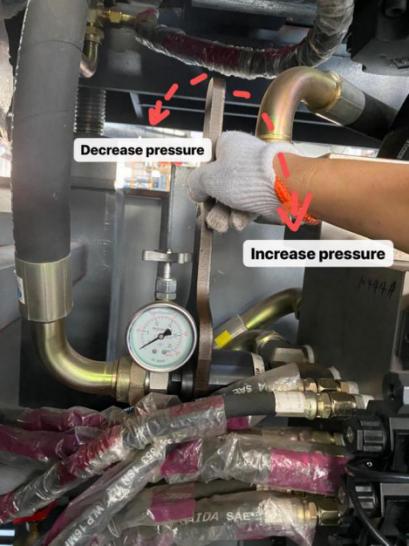
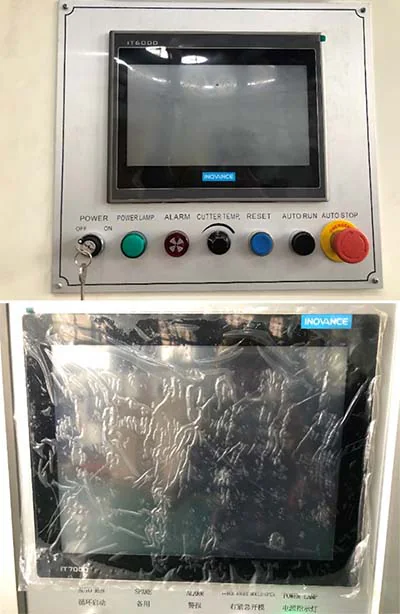
The component illustrations show PLC and touch-screen control, hydraulic valves and parison-control equipment. The interface is used to set, store and monitor operating parameters and display machine faults. Ask for the actual component list and maintenance documentation for the supplied configuration, rather than assuming that every pictured brand is included.
Define how the neck and flash will be finished and how the product will be collected. Automatic deflashing and take-out arrangements can reduce handling steps when they match the mold and container design. Include the conveyor, inspection and downstream interfaces in the project scope.
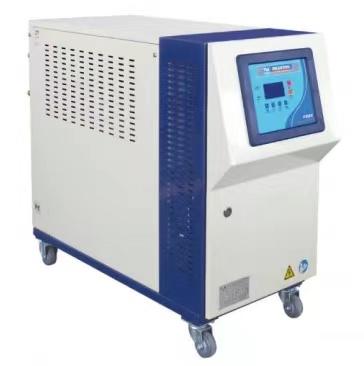
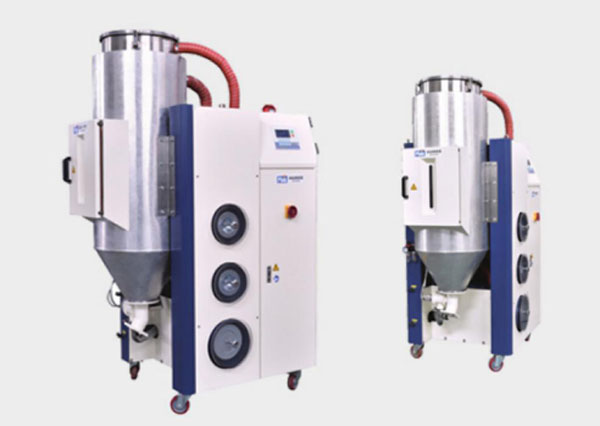
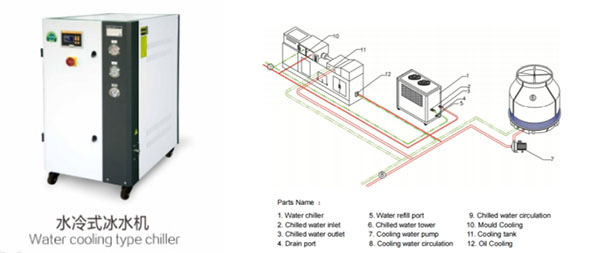
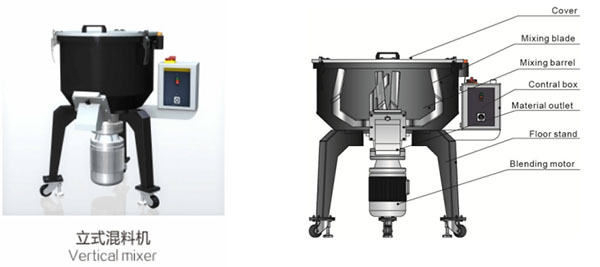
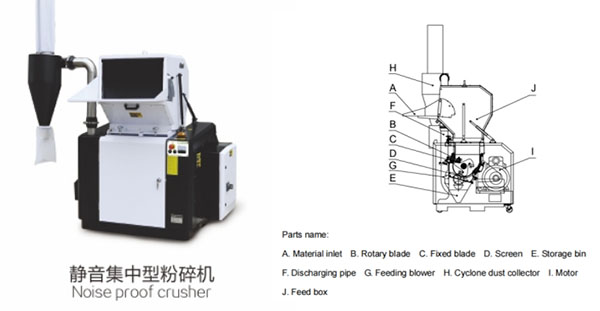
Material loading and mixing, cooling, compressed air and scrap handling all contribute to the production line. The equipment illustrations show autoloaders, mixers, chillers, crushers and air compressors. PC bottle production also includes material drying and mold-temperature control. Size each auxiliary against the actual machine and process requirements.
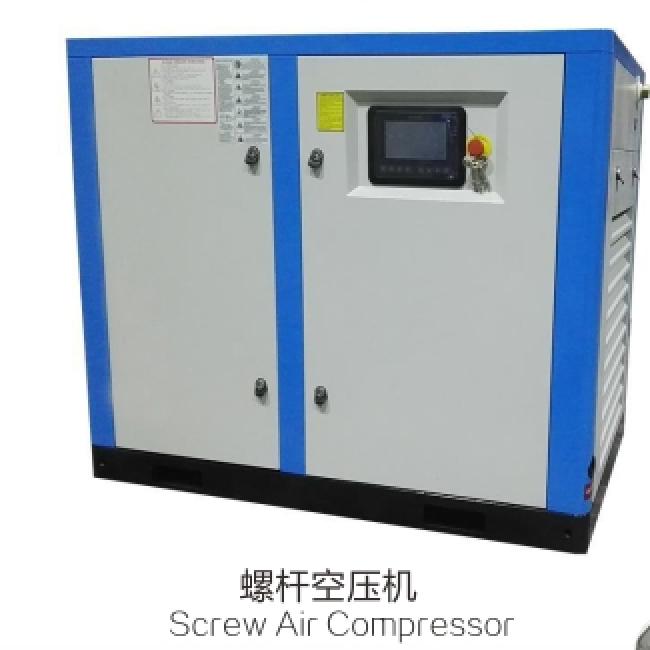
Check the general arrangement drawing, access for installation and maintenance, factory electrical supply, cooling circuit, compressed air and hydraulic requirements. Use the supplied machine documentation for connection and operating values. Installation and adjustments should follow the equipment procedure and be performed by qualified personnel.
Agree the container’s weight, dimensions, neck and closure fit, appearance and required leak or performance checks. The actual contents and distribution conditions determine the acceptance requirements. Record the resin and production conditions used for the trial.
Review the proposed configuration, manufacturing and inspection process, documentation, training, service arrangements and spare parts. Request relevant product videos or a factory discussion, and compare quotations against the same requirements. Include the mold and auxiliaries as well as the machine itself.
Send your drawing or sample, material, volume, target weight, output requirement, head or layer preferences, and factory location. Include any existing tooling and downstream equipment. Continue with the machine selection checklist or the cost planning guide.
This guide covers polycarbonate (PC) bottles; Tritan configurations are also available in the TDB-25APC product range. Specify the grade and drying requirements with the material supplier.
A dedicated extrusion blow molding machine. In the Tongda range this is the TDB-25APC, a single-station machine for 3–5 gallon water bottles.
Drying, moisture control and controlled heating are important parts of PC bottle production. Follow the material supplier's drying requirements and include the dryer in the production line.
In addition to loading, mixing, cooling, compressed air and scrap handling, PC bottle production includes material drying and mold-temperature control. Size each auxiliary for the actual machine and process.
Output depends on the bottle weight and design, material, drying and cooling time. Agree output as accepted bottles per hour for your named bottle in a trial, not as a dry-cycle rate.
The price depends on the machine configuration, the mold, the dryer and other auxiliaries, and handling. Compare quotations against the same container, output and scope; the cost guide lists what to include.
Let's build your next production line
Share your container, material and production requirements. We’ll help you identify a suitable machine configuration.
Discuss your project