Parting line
Where the mold splits decides visible seams and how the part releases.
Manufacture better extrusion blow moulding machines for you.
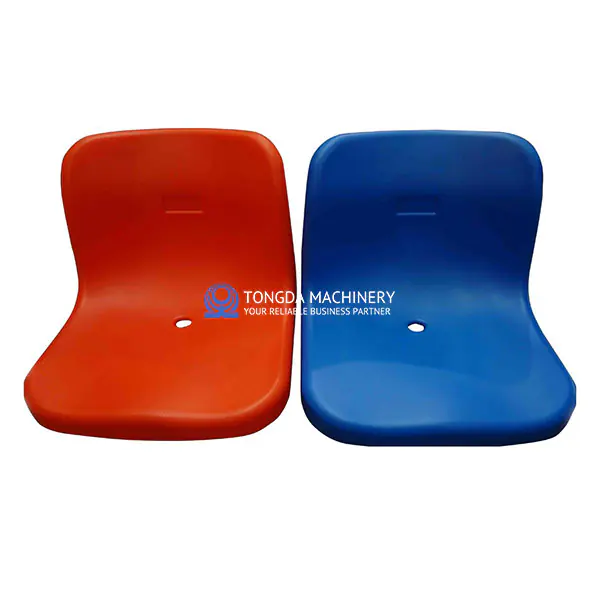
Large & technical parts
Machine and mold configurations for hollow seats, shaped housings and other irregular parts, with published specifications side by side.
In short
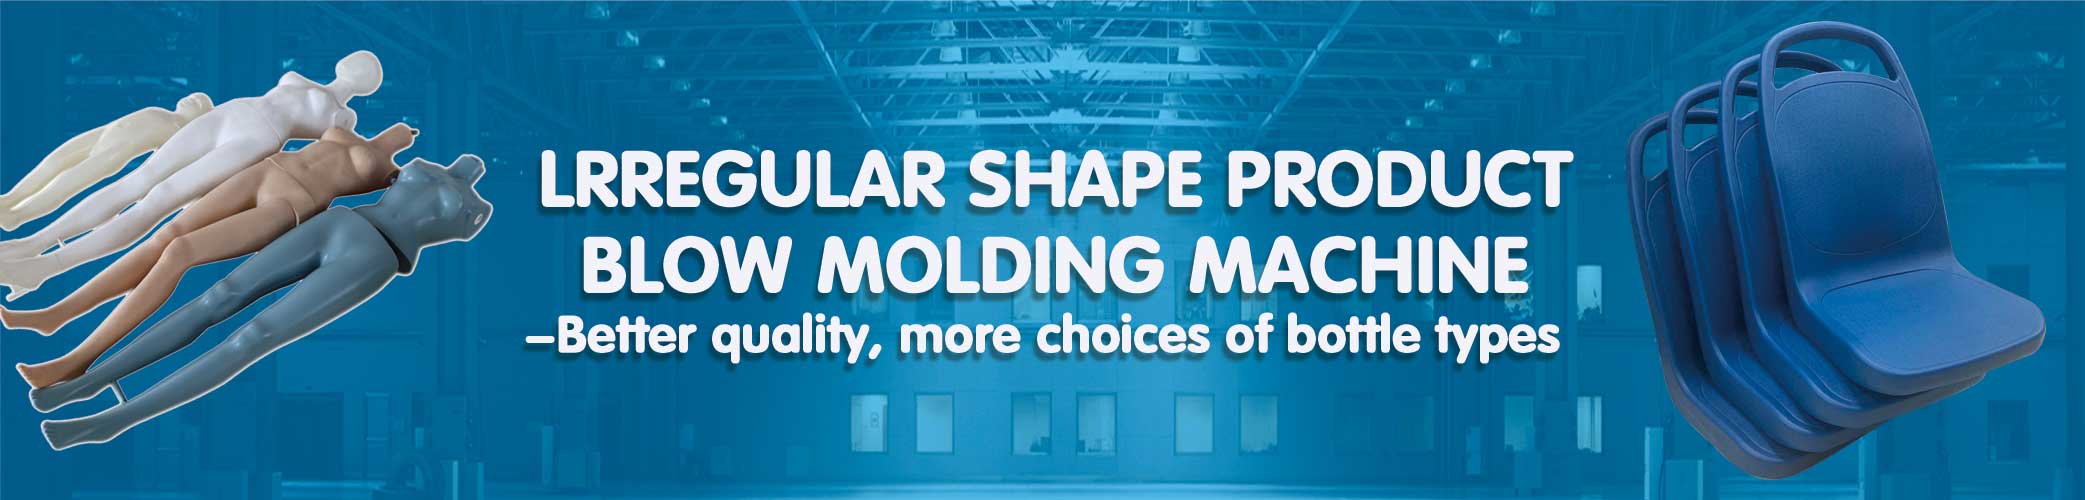
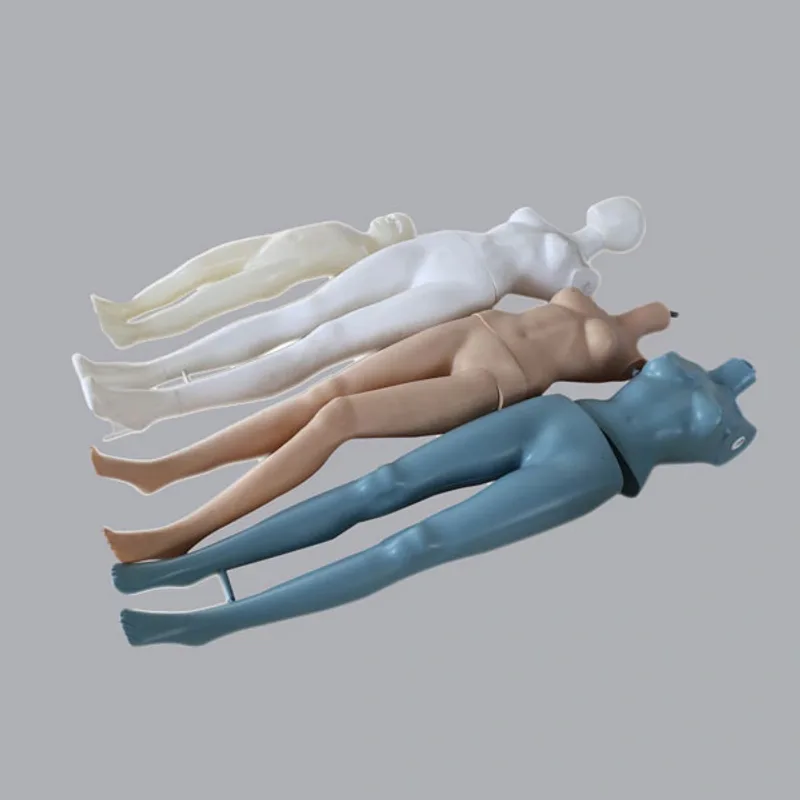
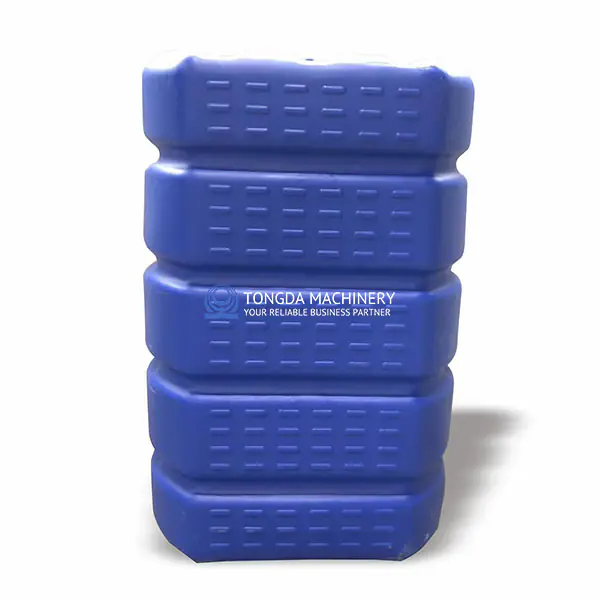
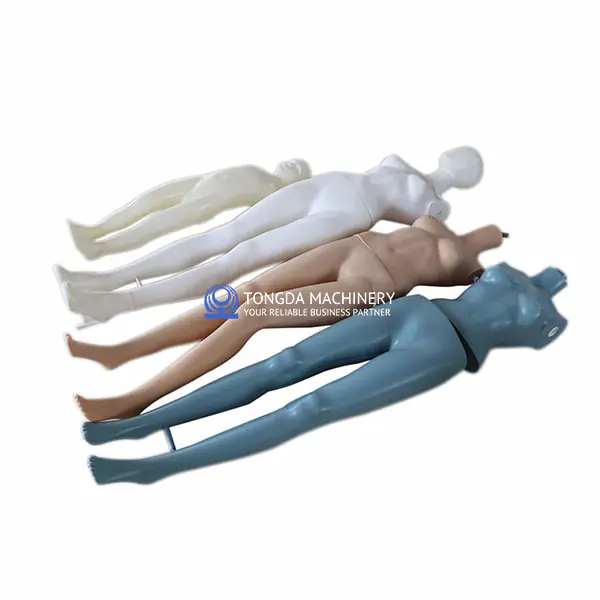
Irregular hollow products, such as mannequins, hollow seats and shaped housings, depend on mold design as much as on the machine. Tongda reviews parting lines, undercuts and wall distribution first, then matches a TDB machine to the part.
Assess parting lines, undercuts, wall distribution and removal from the mold at the start of the project. Tongda’s published application range points to TDB machines for these products.
Production process
Blow-molding grade resin, masterbatch and regrind are dosed to the product specification.
The extruder melts the material and the die head forms a hollow tube of controlled wall thickness.
The mold closes on the parison and compressed air forms the part against the cavity.
The part cools in the mold until it holds its shape, then the mold opens and the part is removed.
Flash at the neck, handle and base is removed; necks are cut or reamed where required.
Weight, dimensions and leak tightness are checked before labeling and packing.
Selection guide
Where the mold splits decides visible seams and how the part releases.
Undercuts may need mold slides or a different orientation.
Deep or stretched areas need parison programming to avoid thin spots.
Plan trimming of complex flash lines and any assembly steps.
Machine configurations
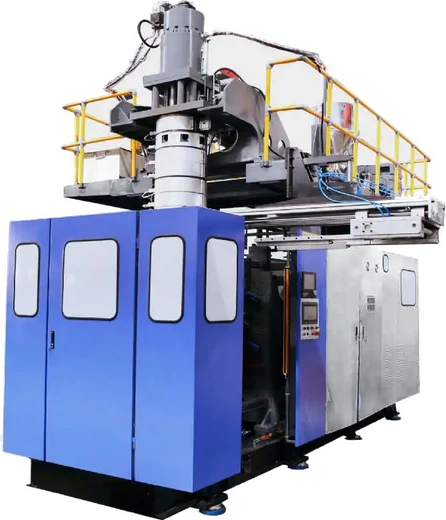
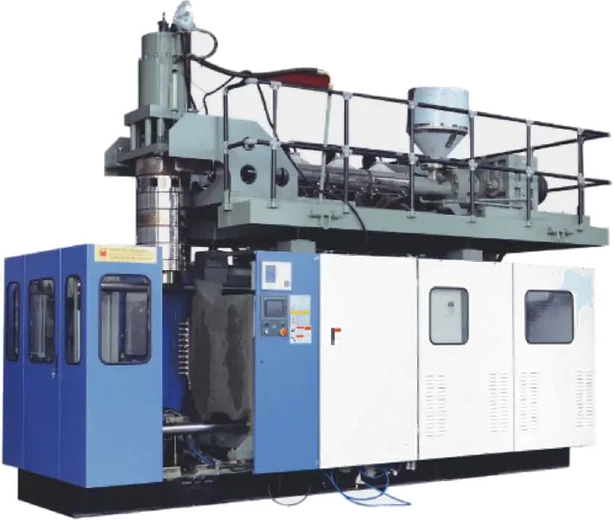
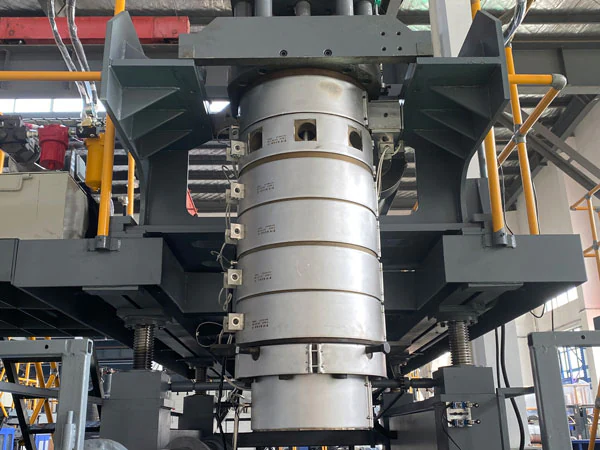
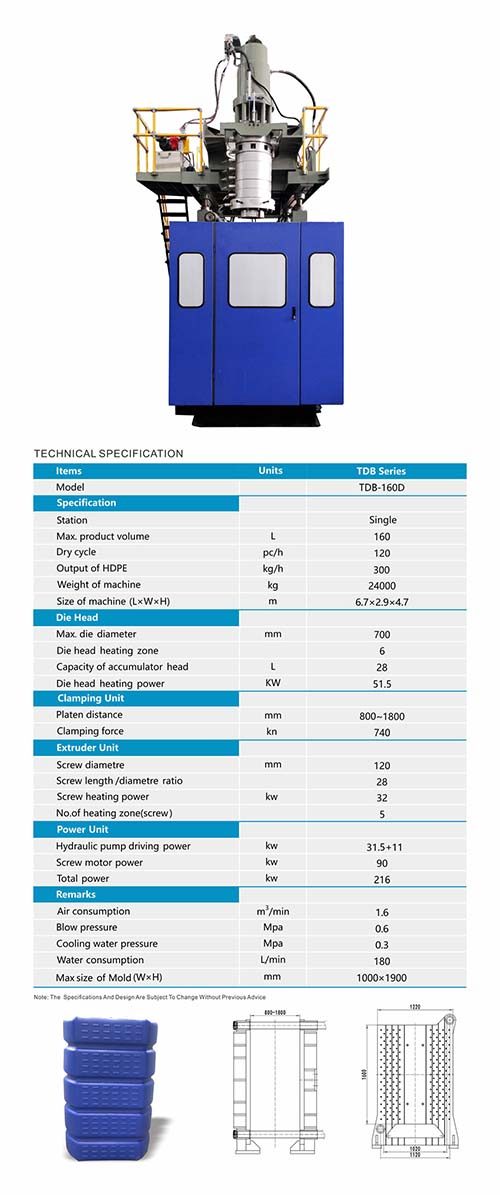
Accumulator-head extrusion blow molding for 50–80 L products, with bottom blowing and a servo motor.
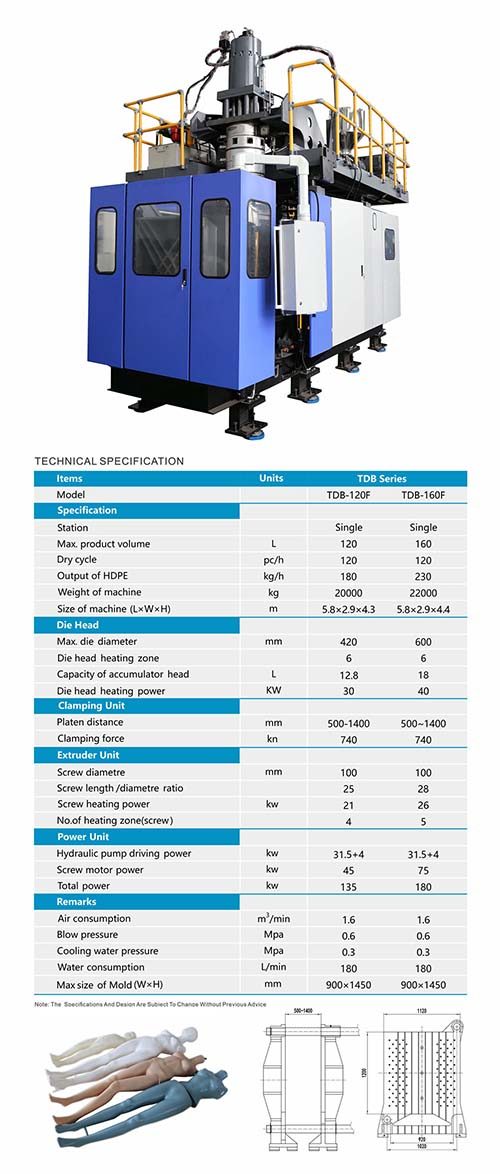
Accumulator-head extrusion blow molding for 80–120 L products, with bottom blowing and a servo motor.
| Model | Stations | Max. volume | Clamping force | Screw | Total power | Max. mold (W × H) | Datasheet |
|---|---|---|---|---|---|---|---|
| TDB-80F | Single | 80 L | 440 kN | 100 mm | 131.5 kW | 800 × 1000 mm | PDF · 2.3 MB |
| TDB-120F | Single | 120 L | 740 kN | 100 mm | 131.5 kW | 900 × 1450 mm | PDF · 2.1 MB |
Suggested starting points from the published range. The final configuration depends on your product drawing, resin, weight and output target.
Quotations, prices and project cases: Tongda irregular-shape product machines on tongdamachine.net ↗
Machine in operation
Watch a Tongda machine producing this type of product, from parison extrusion to the finished part. For a video of a specific model or configuration, ask our team.
More machine videos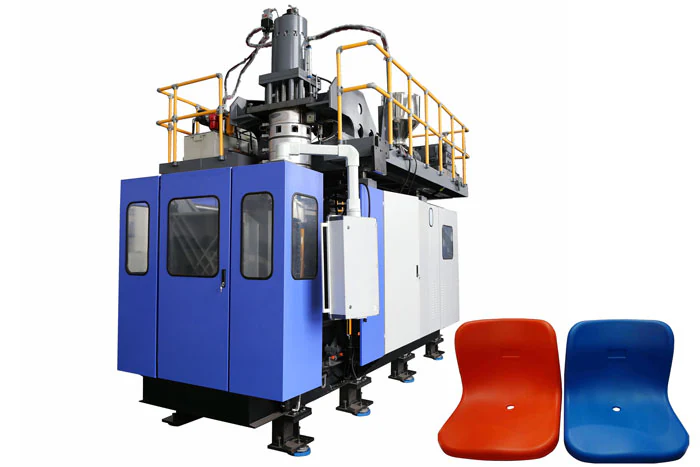
Questions from buyers
Didn't find your answer?
Ask our engineersYes. Mannequins and other shaped hollow products are made by extrusion blow molding with purpose-built molds.
TDB machines such as the TDB-80F and TDB-120F are typical. The size and weight of your part decide the model.
A 3D drawing or sample, the material and the required annual quantity.
Let's build your next production line
Share your container, material and production requirements. We’ll help you identify a suitable machine configuration.
Discuss your project