Controls and drive system
HSE machines are built on a Siemens or Inovance control platform, with the matching touch screen, servo drives and parison wall-thickness control. Confirm the platform and component list in the quotation.
Manufacture better extrusion blow moulding machines for you.
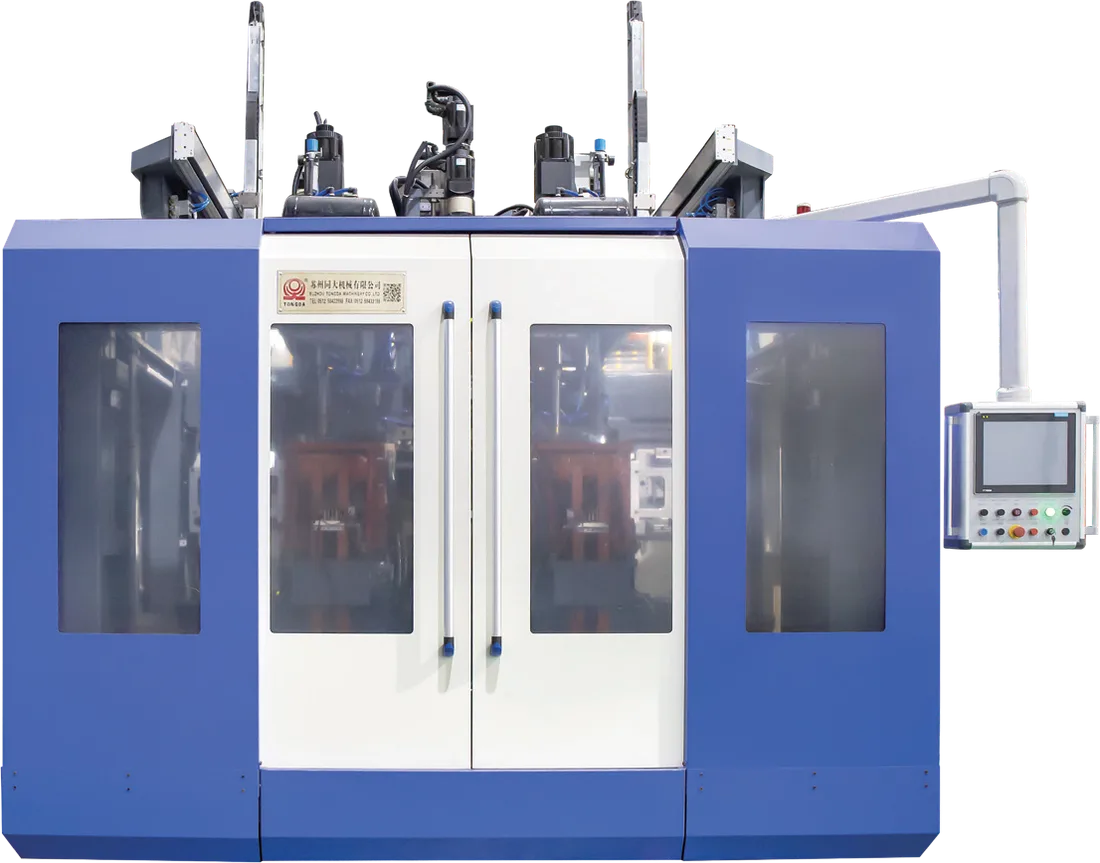
HS Series · Extrusion blow molding machine
Double-station, fully electric extrusion blow molding for bottles and jerry cans up to 5 L, with electric drives for extrusion, mold movement and parison control.
Products description
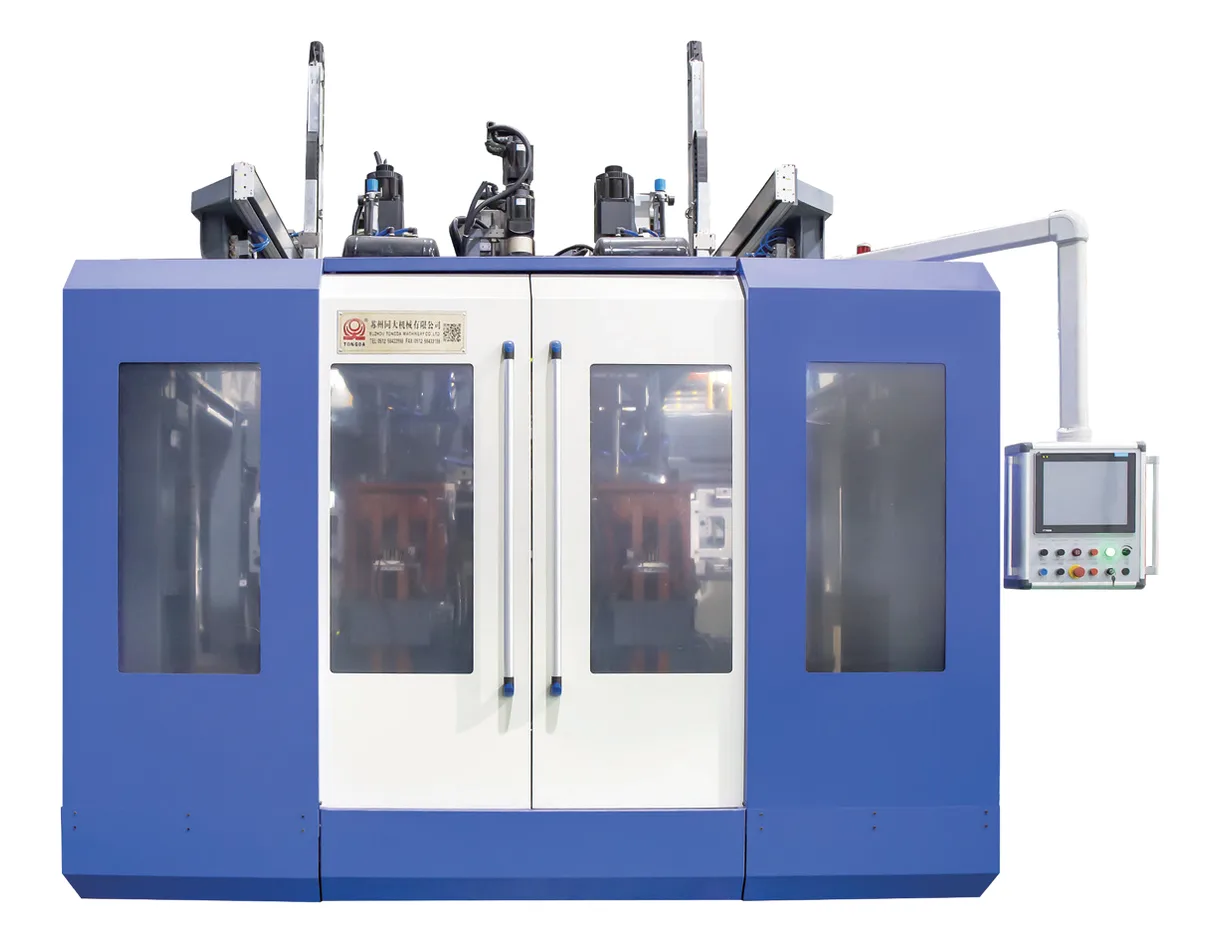
Double-station, fully electric extrusion blow molding for bottles and jerry cans up to 5 L, with electric drives for extrusion, mold movement and parison control. The HSE range is the fully electric version of the Tongda HS series and appears beside it in the 2026 catalogue. Share your bottle or container drawing to discuss the mold, head arrangement and handling requirements.
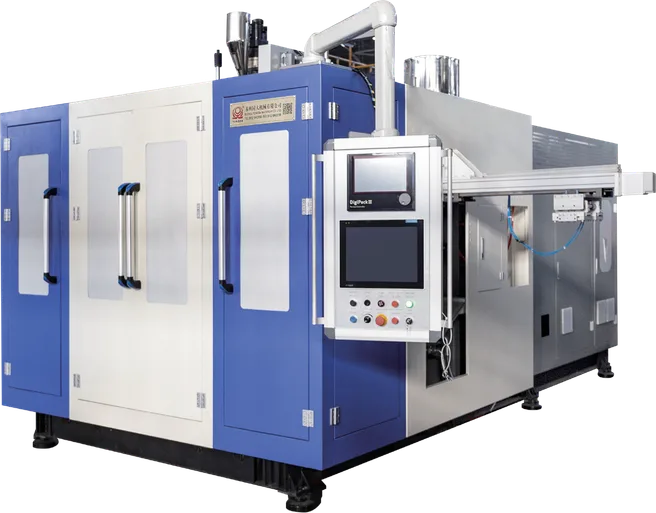
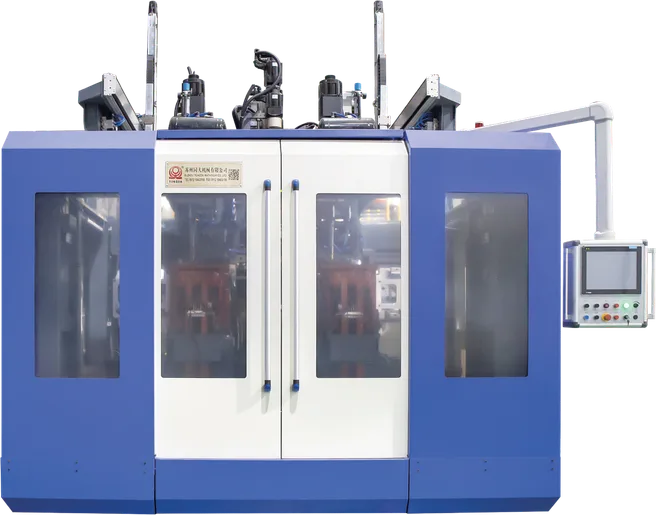
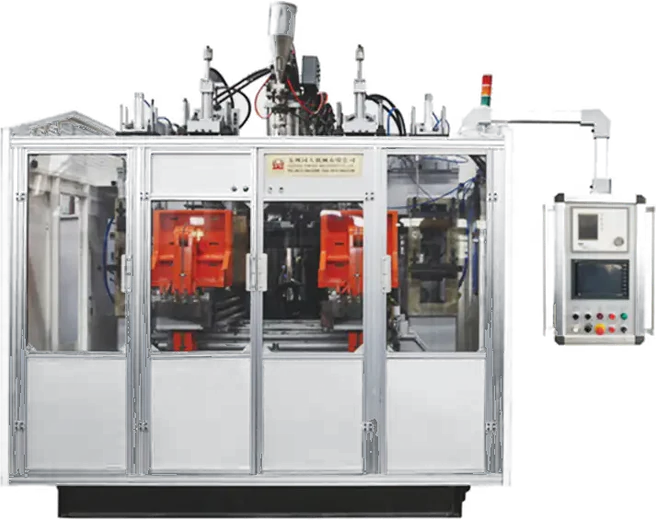
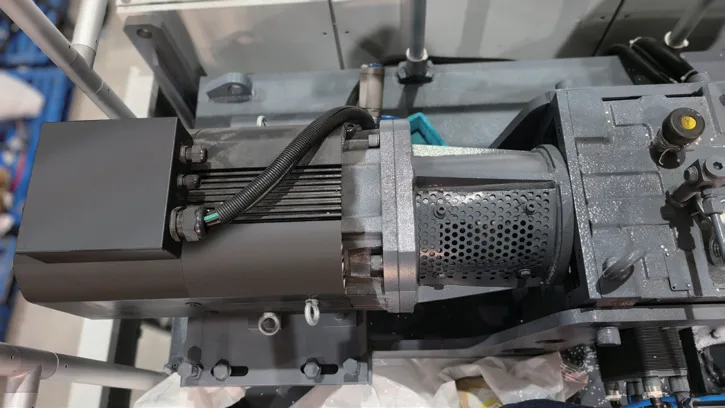
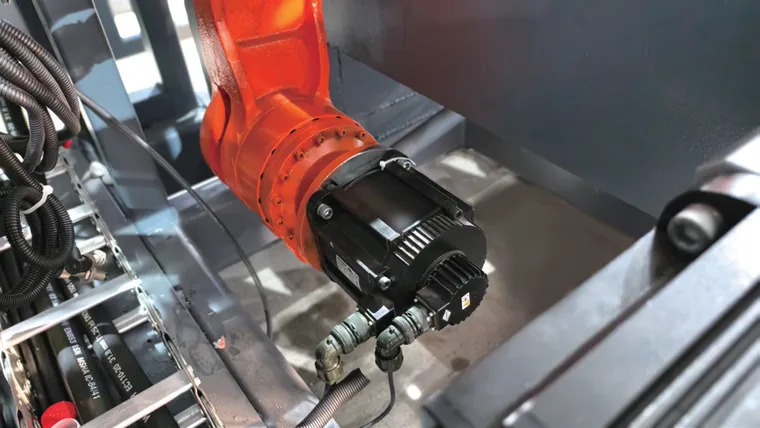
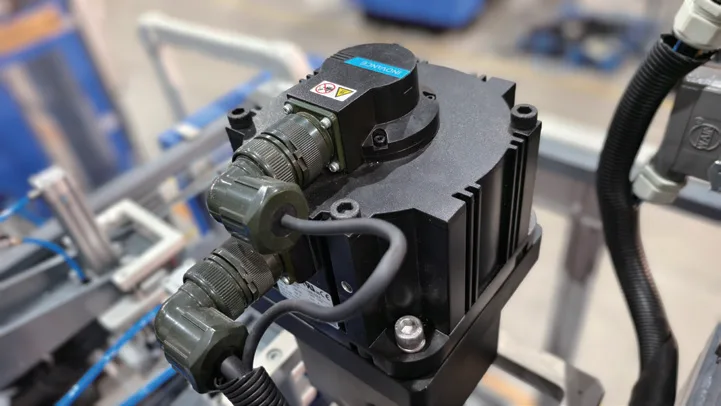
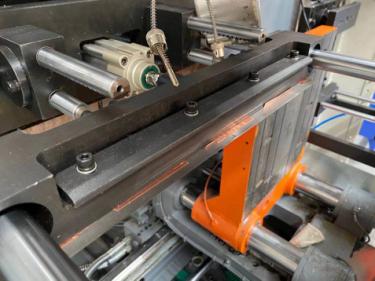
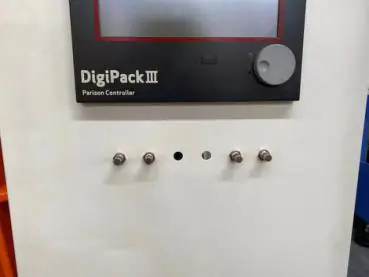
Extrusion, mold opening and closing, and parison wall-thickness control each have an electric drive unit, shown in the photos below. The specification lists no hydraulic pump power: the machine has no hydraulic power unit, so there is no hydraulic oil to supply, cool or maintain.
HSEII-5L
| Stations | Double |
|---|---|
| Stated maximum product volume | 5 L |
| Dry cycle | 1,600 pc/h |
| HDPE output | 130 kg/h |
| Machine weight | 22,000 kg |
| Machine dimensions (L × W × H) | 7.1 × 4 × 4.5 m |
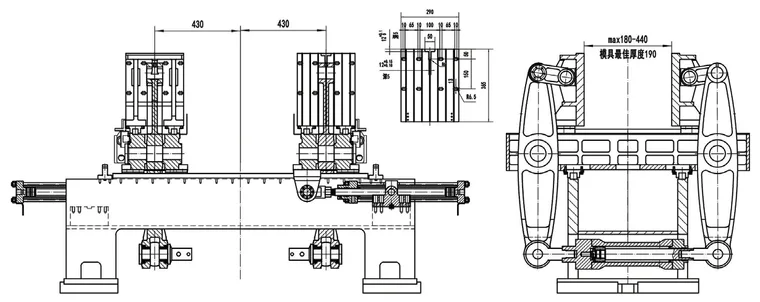
| Clamping force | 158 kN |
| Screw diameter | 90 mm |
| Installed total power | 106.9 kW |
| Maximum mold size (W × H) | 540 × 430 mm |
The figures reproduce the 2026 catalogue. The dry cycle is the machine cycle without a product, and HDPE output is the extruder’s plasticizing capacity; finished-product output depends on resin, weight, cavity arrangement, cooling and the production cycle. Installed power is connected equipment power, not measured energy use.
Source: Tongda 2026 catalogue (edition 20260818), pages 21–22. Download the catalogue.
Published machine information is a starting point for selection. Final configuration and performance depend on your product, material, mold and operating conditions.
Configuration & components
| Component | Siemens platform | Inovance platform |
|---|---|---|
| PLC | Siemens | Inovance |
| Touch screen (HMI) | Siemens | Inovance |
| Inverter | Inovance or Siemens | Inovance |
| Servo motors (blow pin, deflashing, robot) | Siemens | Inovance |
| Parison wall-thickness controller | Siemens system integration (not with the Siemens SMART platform) | Inovance system integration |
Fully electric: extrusion, mold movement and parison wall-thickness control use electric drives, with no hydraulic power unit.
What it makes
The HSEII-5L is configured for hollow products up to 5 L. Bottles and containers made on HSE machines.
Explore applicationsInside the machine
HSE machines are built on a Siemens or Inovance control platform, with the matching touch screen, servo drives and parison wall-thickness control. Confirm the platform and component list in the quotation.
Working with Tongda
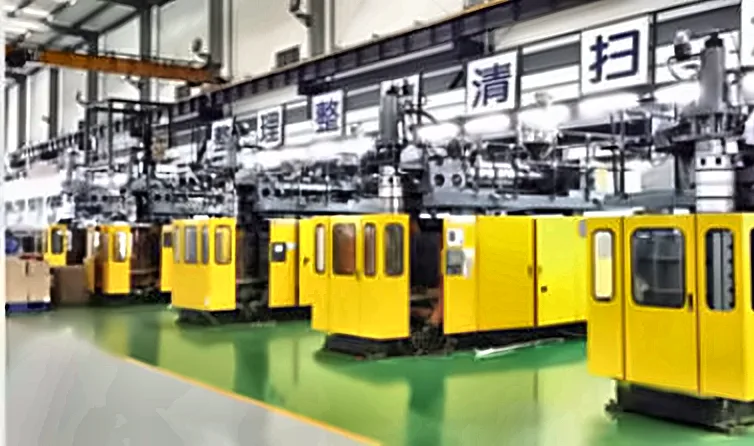
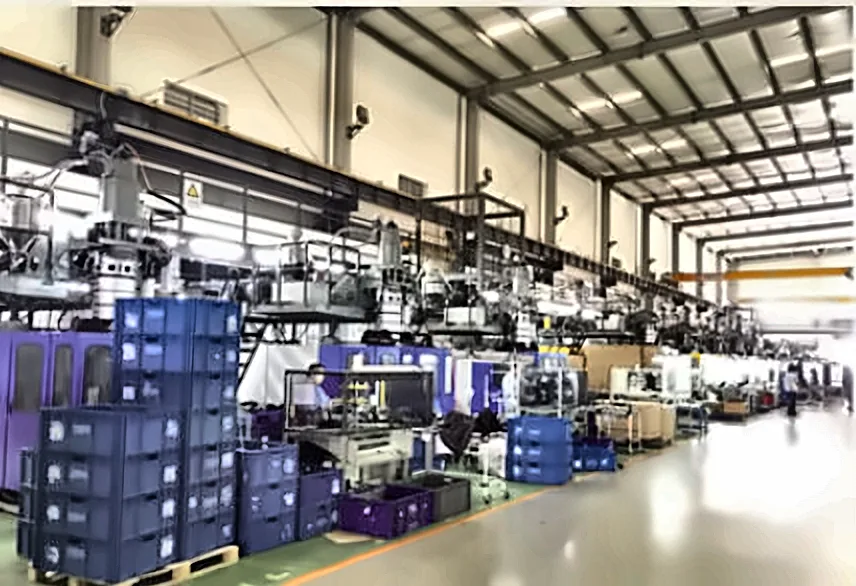
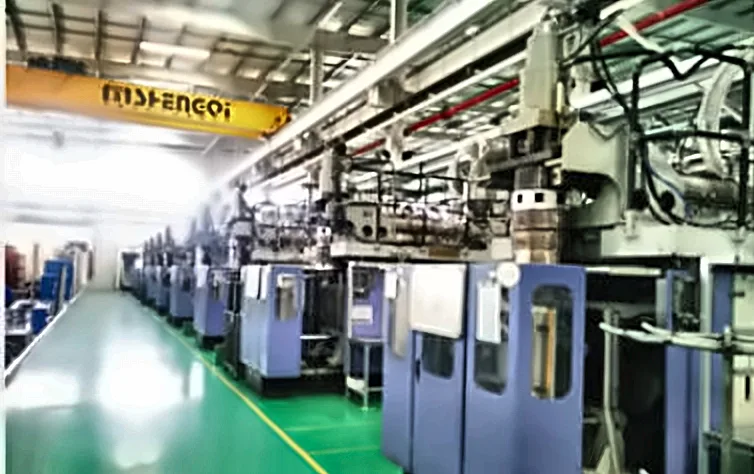
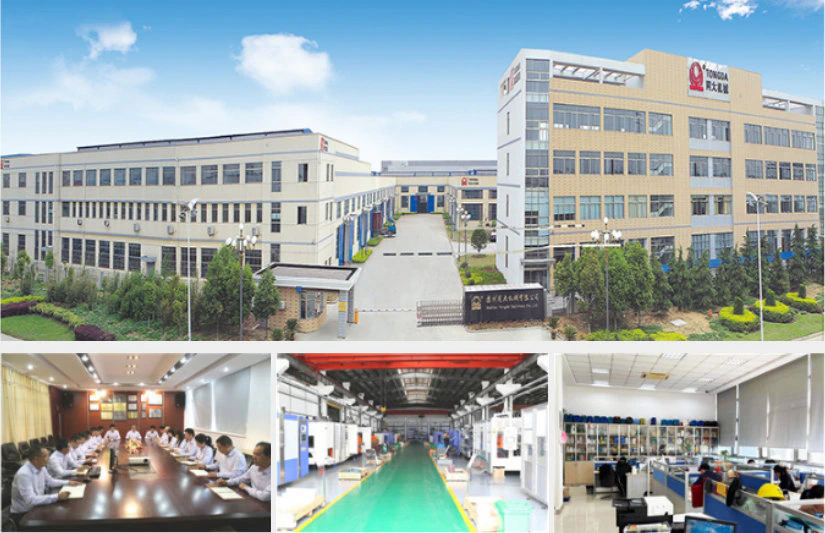
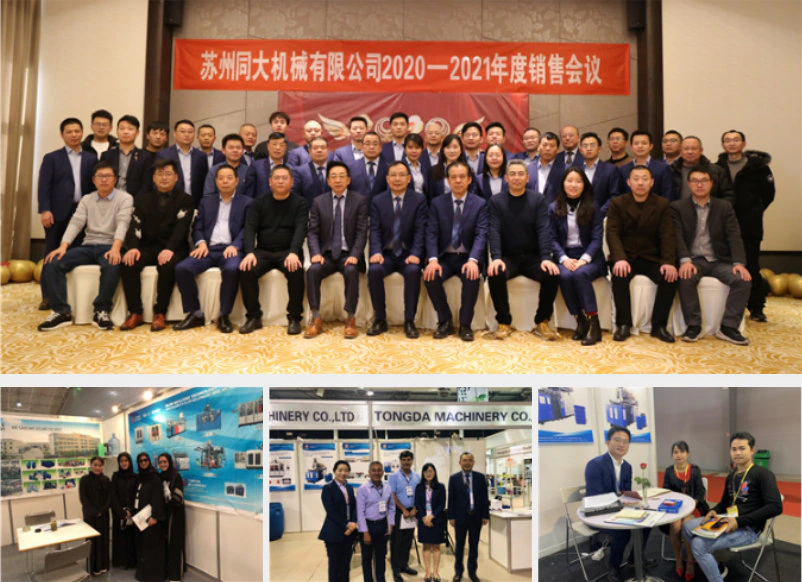
Founded in 1999, Suzhou Tongda Machinery Co., Ltd. provides complete-plant smart manufacturing solutions centered on extrusion blow molding equipment. Its headquarters is at No. 21 Fenghuang Avenue, Zhangjiagang, Suzhou, Jiangsu.
Tongda operates three manufacturing plants covering approximately 100,000 square meters, with annual production capacity exceeding 1,200 machines and systems. For 15 consecutive years it has ranked among the top three companies in China’s extrusion blow molding machinery sector.
As of 2025, Tongda has contributed to six national standards, one industry standard and one association standard, and holds more than 90 national patents. “Growing with Partners” is the spirit of Tongda; new and existing customers are warmly welcome to visit.
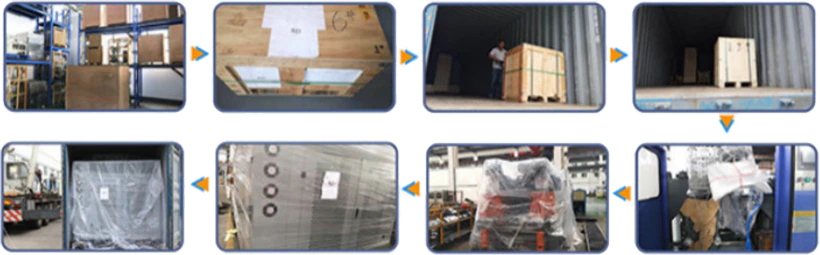
Machines shipped overseas are normally packed in wooden cases, chosen according to the dimensions of the main machine. We can also pack machines to meet specific customer requirements. As a professional blow molding machinery company, Tongda will do its best to meet every customer's needs.
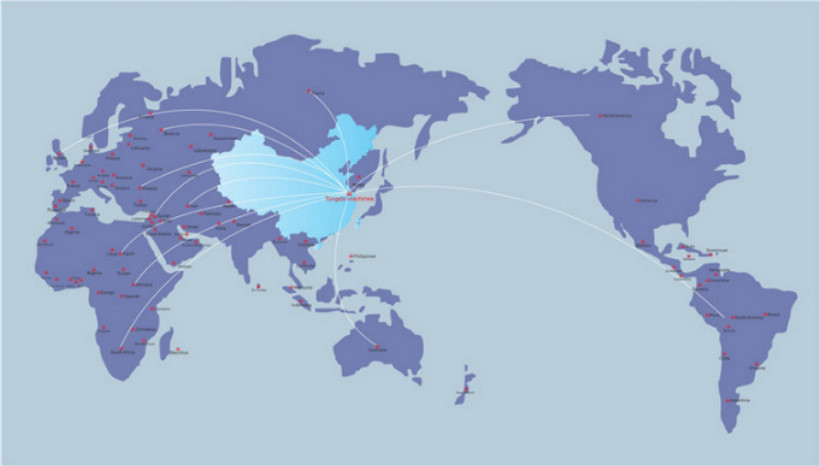
More than 10,000 Tongda machines and systems have been supplied to customers in over 100 countries and regions.
A network of 27 overseas and 14 domestic sales and service centers provides professional support 24 hours a day, seven days a week.
Customers include manufacturers in the United States, United Kingdom, Australia, Poland, Russia, Mexico, Brazil, Saudi Arabia, the UAE, Indonesia, Ethiopia, Nigeria and Chile. We provide not only high-quality machines but also fast, timely service to every customer.
Customer success is the goal of every member of the Tongda team; the only way we compete is by helping customers meet their requirements.
Questions from buyers
Answers to common questions about selecting, configuring and running Tongda extrusion blow molding machines.
Didn't find your answer?
Ask our engineersSmall continuous-extrusion machines are normally available as single- or double-station models. The difference is output: a single-station machine spends more of each cycle on mold movement out and back.
Output depends on the product volume, its widest diameter and the mold cooling conditions. Please send the product dimensions and weight first; we will recommend a suitable mold material for your requirements.
For oil-can style containers: 1 L conventional about 70 g; 4 L about 180–200 g; 5 L about 200–240 g.
Yes. Our equipment can be configured for automatic flash removal.
The result depends on the mold, the mold material and the product shape. We will recommend the best scheme for your machine.
Yes.
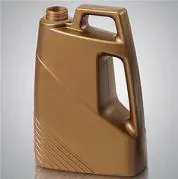
Conventional products use a cold cutter, which is easier to handle. For in-mold labeling, thinner-walled products, or PP, PVC and PETG materials, a hot cutter is more suitable.
For wide-mouth bottles, larger-diameter jars and products that will be heat-sealed later, we recommend a rotary-cut neck.
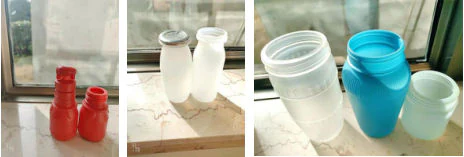
Yes, depending on the angle. Please send product pictures so we can confirm.
Yes. We can engrave the mold with your logo, company name, date, number, telephone and other details to order.
Yes. Based on your bottle shape and labeling requirements we recommend a suitable labeling method, such as in-mold labeling, self-adhesive labeling or hot-melt labeling.
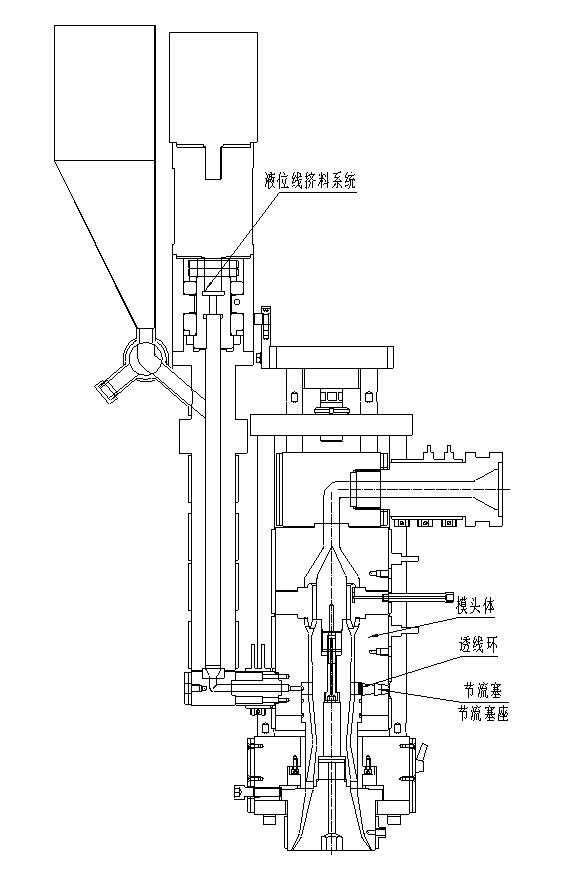
The height of the liquid in a container is its liquid level. A transparent stripe on the container that shows this level is called a liquid level line, and it makes the contents easy to check.
The level lines we commonly use are Φ22 and Φ30. Φ22 is installed on the die head; Φ30 is installed on the plasticizing system.
Yes, it can be added later. On a single die-head machine, replace the die head body, fit a through ring, add a throttle plug and throttle plug seat, and install an extrusion system. On a multi-head machine, the die body, through ring, throttle plug and seat are needed for each die head.
Please send the specific information of your existing molds. Our engineers will confirm whether they can be installed directly on our machine.
First make sure the parison hangs straight front to back, then adjust the two adjustment screws behind the die.
Polish the die sleeve.
1) If the die pre-blow is too strong, reduce it.
2) If the mold temperature is too low, raise it.
3) If mold venting is insufficient, add mold vents.
1) If the clamping pressure is too low, increase it.
2) If the mold flash grooves are too shallow, deepen them.
3) If the mold is not flat, adjust it.
4) If the platen is not flat, adjust it.
1) The clamping speed is too fast: adjust the process time and close the mold more slowly.
2) The mold pinch-off edge is too sharp or has burrs: repair the edge.
3) The handle shape is unsuitable: the process was not considered in the mold design.
4) The die is too small or the pre-blow too weak: enlarge the die or adjust the pre-blow.
5) The parison is not round or has wrinkles: remake the die and increase die pressure.
6) The mold temperature is too high, so material breaks when the mold closes: control mold temperature with cooling water and a chiller.
7) For handles blown inside the mold: the in-mold blow needle may be too short, or it may fire too early or too late; the blow-needle cylinder design may also be unsuitable. A blow-while-piercing cylinder uses a single action and is less stable; a pierce-then-blow cylinder is more stable but needs a longer mold opening and closing stroke on the machine.
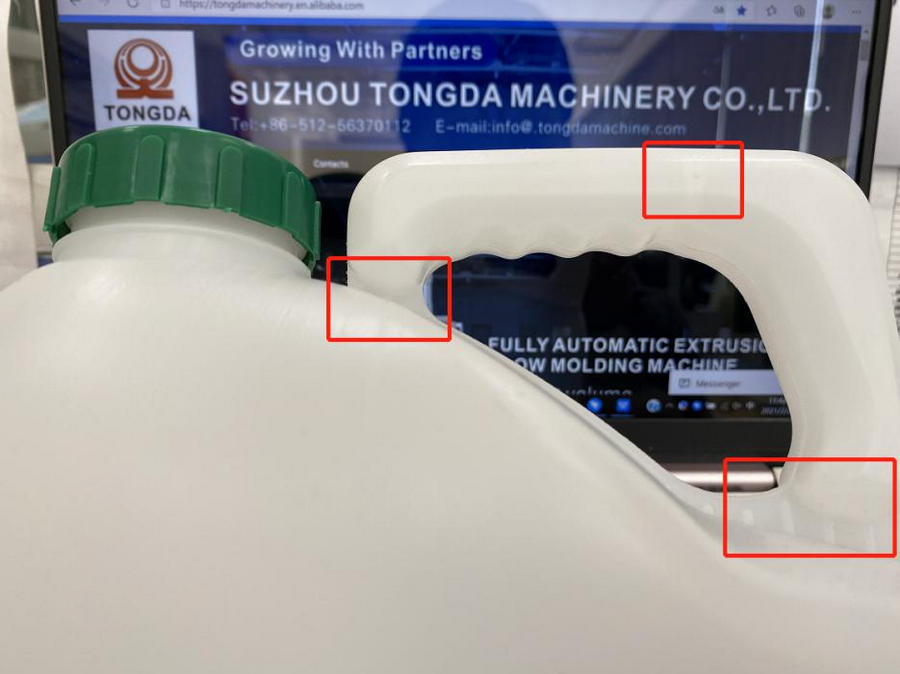
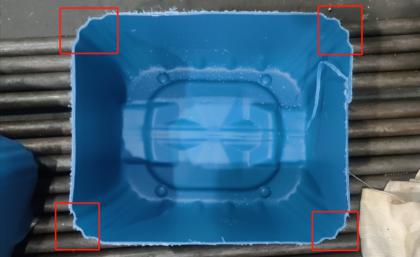
1) Adjust the corresponding wall thickness (the effect is limited).
2) Modify the die at the four corners. The parison leaves the die with a uniform wall, so for a square product with stretched corners, material must be added at the matching corners of the die — usually by reworking the die sleeve; a segmented die core can also be reworked.
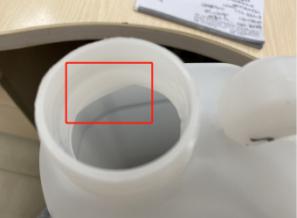
1) The cutter did not cut cleanly and the neck did not open when the blow needle descended, dragging material. Check whether the blade is blunt or damaged and whether its fixing screws are loose; die pre-blow and constant blowing can also contribute.
2) The blow needle is the wrong size: modify it.
3) The pinch-off edge angle is wrong or its diameter is too small: modify the mold edge.
4) The process timing is wrong: adjust the pre-blow time and the blow needle's descending speed.
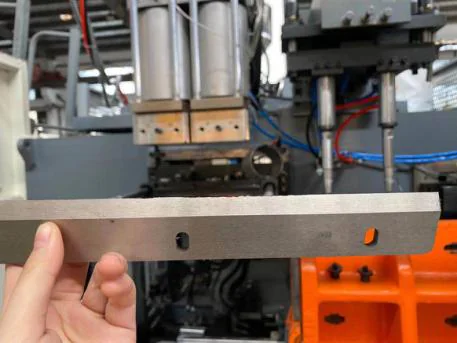
1) Correct any abnormal die shape.
2) The product is not cooled enough: lower the cooling water temperature or extend the cycle.
The standard warranty is 14 months from shipment from the factory. During the warranty period, parts that fail without misuse or accidental damage are replaced.
Operator training and factory layout planning are included. Installation and commissioning are quoted separately, so ask for them as a line item in your quotation.
The HT, HTS, HW, HWS, HS, HSE, EH, ME, CF, TDY, TDB, TDW, TDBS and TDBX series are covered by a Machinery Directive 2006/42/EC attestation of conformity issued by UDEM International Certification (certificate M.2025.206.C121093, valid until 19 June 2030), assessed against EN ISO 12100, EN 422 and EN 60204-1.
Machines are built on a Mitsubishi, Siemens or Inovance control platform, depending on the series and your choice. The parison wall-thickness controller is MOOG on the Mitsubishi platform and system-integrated on the Siemens and Inovance platforms. Hydraulic valves are Yuken and hydraulic pumps are Sumitomo. Each machine page lists the platforms available for its series.
No. Tongda builds extrusion blow molding machines for HDPE, PP, PVC, PC and similar materials, from small bottles to 250 L drums, IBC tanks and large panels.
Continue exploring
Single-station hydraulic servo extrusion blow molding for bottles and jerry cans up to 5 L, with a toggle clamping unit.
Single-station, fully electric extrusion blow molding for bottles and jerry cans up to 5 L, with electric drives for extrusion, mold movement and parison control.
Hydraulic servo extrusion blow molding for jerry cans, with multi-head configurations for smaller bottles.
Let's build your next production line
Share your container, material and production requirements. We’ll help you identify a suitable machine configuration.
Discuss your project