Milk Bottle Lines: Machine Configurations
Compare multi-head HTS configurations for HDPE milk bottles: stations, heads, clamping force, mold size and downloadable datasheets.
ExploreManufacture better extrusion blow moulding machines for you.
Application engineering guide
How HDPE milk bottles are made, which multi-head machines fit, and what to specify for the neck finish, trimming and quality checks.
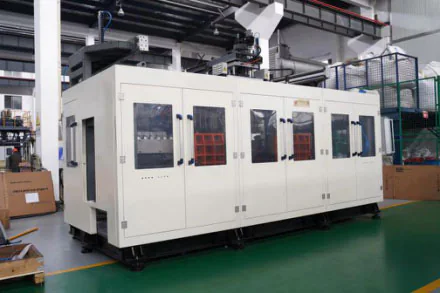
HDPE milk bottles are made by extrusion blow molding on multi-head machines. Several parisons are extruded side by side, the mold closes around them and compressed air forms the bottles. After cooling, the neck is finished by cutting or deflashing and the bottles are checked before they go to filling.
| Machine | Stations | Configuration |
|---|---|---|
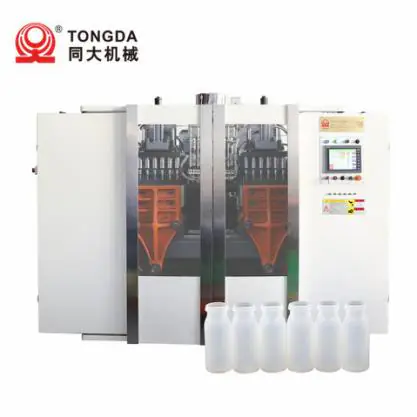
| HTSII-3L | Double | Four- or six-head arrangements for milk and other small bottles |
| HTII-2L, HTSII-2L | Double | Small bottles up to 2 L (stated maximum volume) |
| HT-2L, HTS-2L | Single | Small bottles up to 2 L (stated maximum volume) |
Configurations and specifications: milk bottle line configurations · Quotations and project cases: Tongda milk bottle machines (tongdamachine.net)
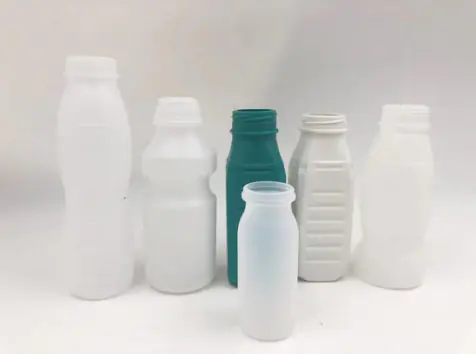
Making milk bottles involves the material, extrusion system, mold, blow pin, cooling, trimming and downstream handling. Begin with a drawing or sample and define the nominal volume, dimensions, target weight, neck, handle and intended use. Those details provide a better basis for machine selection than the volume alone.
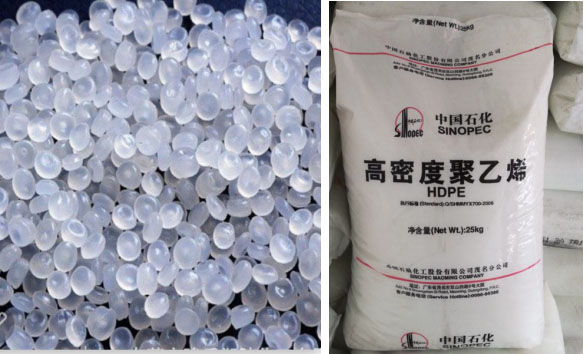
The application range uses HDPE. Specify the resin grade, color masterbatch and any permitted regrind content against the finished container requirements. A material blend is a project decision: it depends on the container’s contents, appearance, physical requirements and the customer’s specification.
The extrusion system melts the material and forms a hollow parison. The mold closes around the parison, air forms it against the mold cavity, and the part cools before removal. The neck and flash are finished according to the tooling arrangement. The material, parison program, mold and cooling must be tuned together during a production trial.
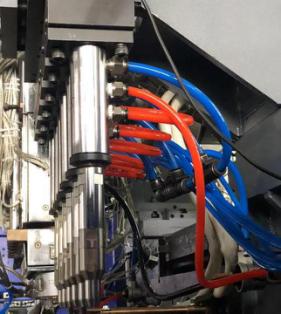
Milk bottle selection depends on bottle width and weight, neck design, head spacing and cavity arrangement. The milk-bottle configurations include six- and eight-head layouts. The HTSII-3L range includes four- or six-head arrangements; discuss the complete configuration for your particular bottle.
| Model | Stations | Stated maximum volume | Clamping force |
|---|---|---|---|
| HTSII-3L | Double | Discuss head and bottle configuration | 70 kN |
Agree output in accepted containers per hour for a named bottle, resin, weight and cavity arrangement. A dry-cycle rate does not include the complete production process. Cooling, extrusion, wall thickness, trimming and downstream handling affect finished-product output. Use an agreed trial to establish the result for the project.
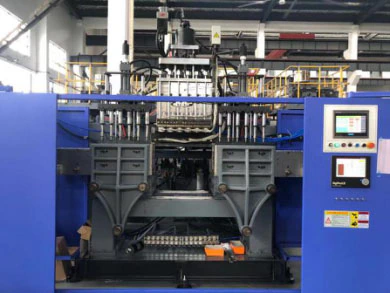
The extrusion-system details identify the gearbox, screw, barrel and driving motor as key components. The screw and barrel affect melting, mixing and delivery of material to the head. Select the configuration for the resin and product requirement; compare the component specification and the supplier’s trial evidence.
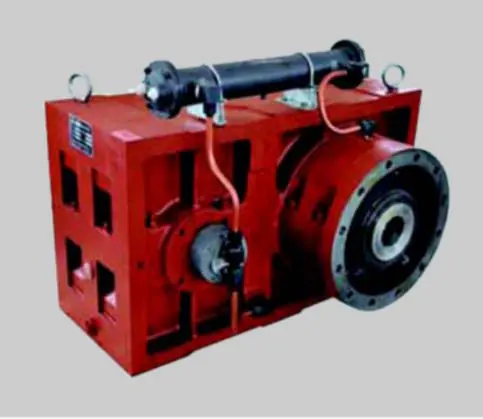
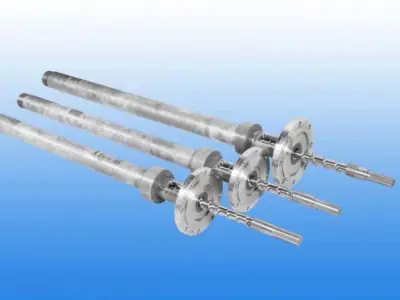
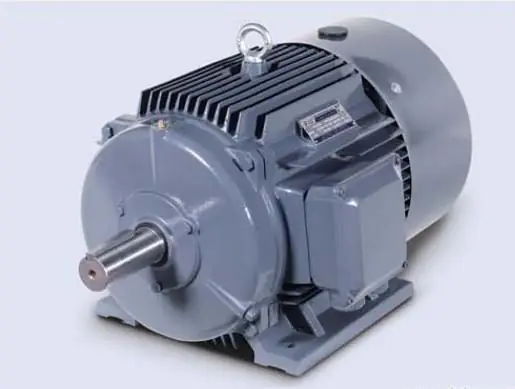
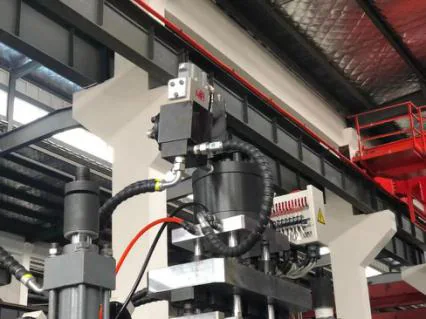
The die head forms the parison from the plasticized material. Its flow path and tooling need to suit the material, product geometry and head arrangement. A parison-control system varies wall distribution along the parison. Evaluate the finished bottle sections, weight and required performance when setting the program during commissioning.
Review the mold’s external dimensions, required opening and mounting arrangement with the machine specification. The machine range shows guided mold movement, toggle clamping and different blow-pin arrangements. Select clamping force and mold support around the actual part and tooling; a larger force alone is not a substitute for a suitable mold design.
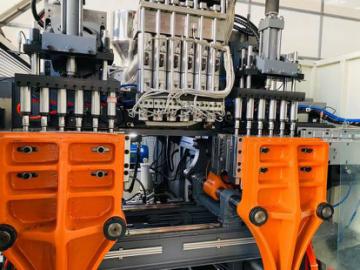
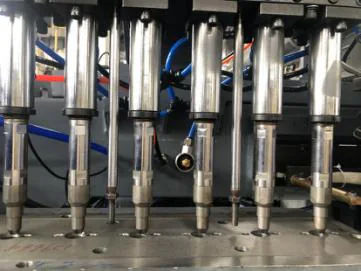
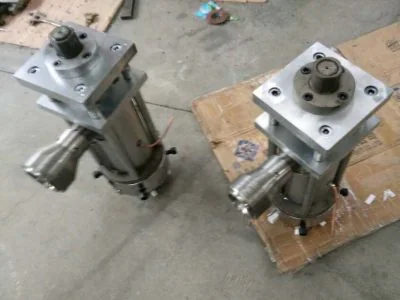
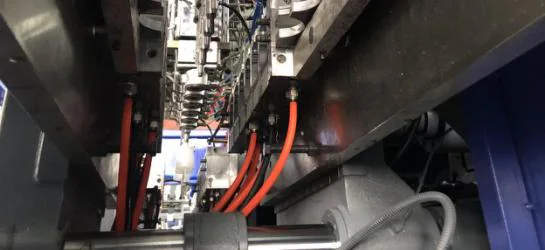
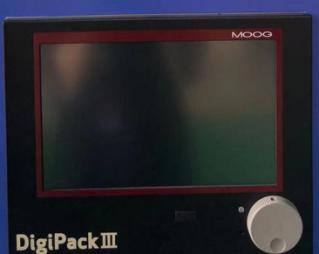
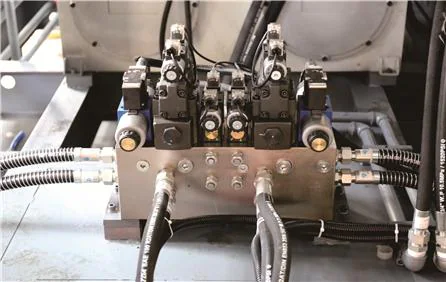
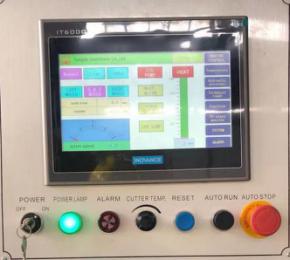
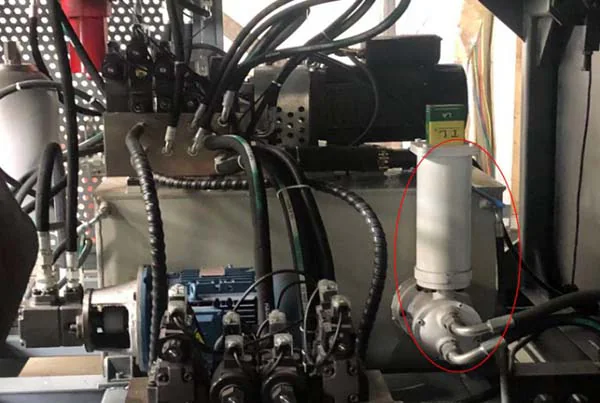
The component illustrations show PLC and touch-screen control, hydraulic valves and parison-control equipment. The interface is used to set, store and monitor operating parameters and display machine faults. Ask for the actual component list and maintenance documentation for the supplied configuration, rather than assuming that every pictured brand is included.
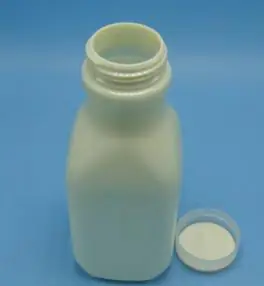
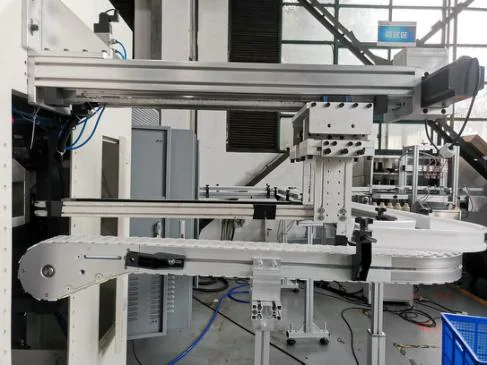
The neck finish determines whether rotary cutting or deflashing is suitable. Review the finished neck and closure fit on the trial bottle. A take-out device and conveyor can link bottle production with leak testing or other downstream equipment; agree these interfaces as part of the production line.
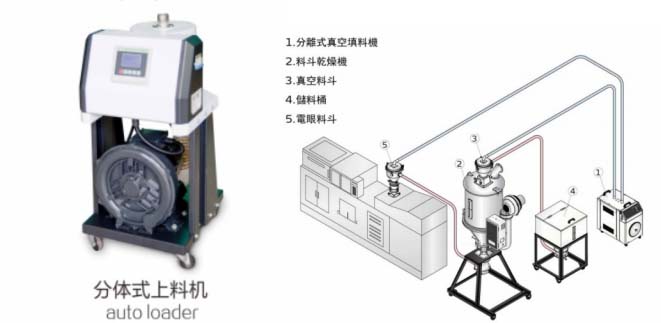
Material loading and mixing, cooling, compressed air and scrap handling all contribute to the production line. The equipment illustrations show autoloaders, mixers, chillers, crushers and air compressors. PC bottle production also includes material drying and mold-temperature control. Size each auxiliary against the actual machine and process requirements.
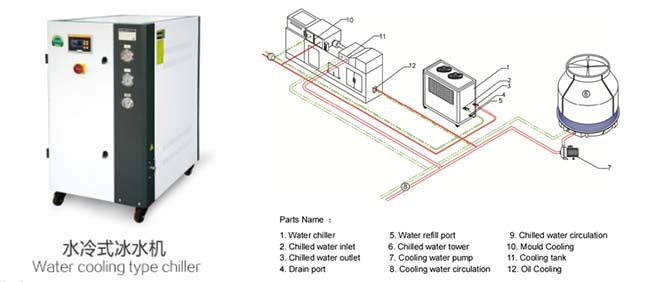
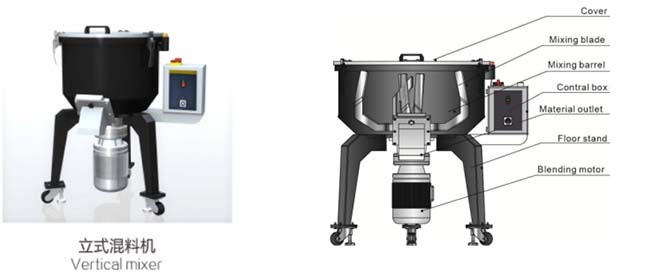
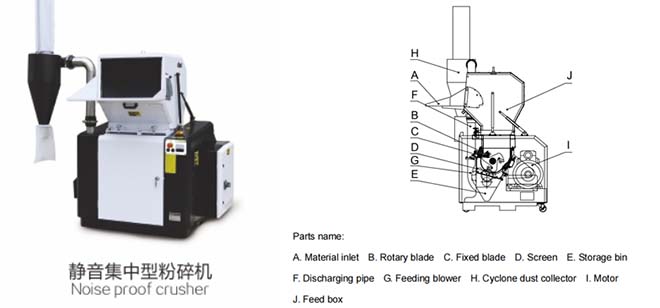
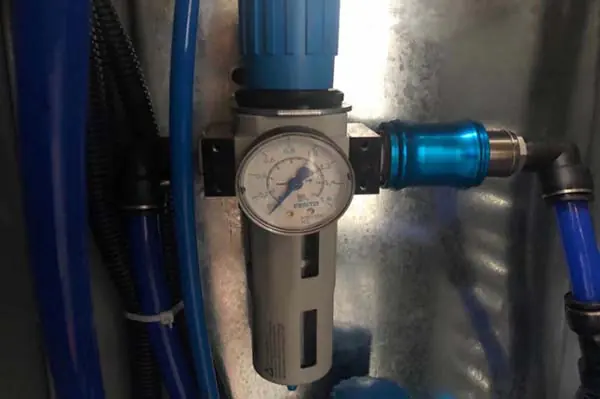
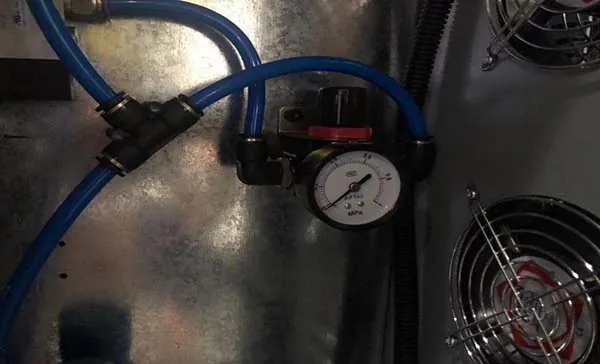
Check the general arrangement drawing, access for installation and maintenance, factory electrical supply, cooling circuit, compressed air and hydraulic requirements. Use the supplied machine documentation for connection and operating values. Installation and adjustments should follow the equipment procedure and be performed by qualified personnel.
Agree the bottle weight, dimensions, neck and closure fit, appearance and leak checks. Define any additional requirements for the intended dairy packaging application with the relevant product and material specifications.
Review the proposed configuration, manufacturing and inspection process, documentation, training, service arrangements and spare parts. Request relevant product videos or a factory discussion, and compare quotations against the same requirements. Include the mold and auxiliaries as well as the machine itself.
Send your drawing or sample, material, volume, target weight, output requirement, head or layer preferences, and factory location. Include any existing tooling and downstream equipment. Continue with the machine selection checklist or the cost planning guide.
Blow-molded milk bottles in this range are made of HDPE. Specify the resin grade and masterbatch with the material supplier against the dairy packaging requirements.
A multi-head extrusion blow molding machine. In the Tongda range the HTSII-3L is offered with four- or six-head arrangements, and milk-bottle configurations include six- and eight-head layouts.
It depends on the bottle width and weight, the neck design, head spacing and the cavity arrangement the mold allows, as well as the output you need. Discuss the complete configuration for your bottle.
The neck finish determines whether rotary cutting or deflashing is suitable. Check the finished neck and closure fit on trial bottles before the configuration is fixed.
Output depends on the bottle size and weight, number of heads and cavities, and cooling time. Agree output as accepted bottles per hour for your named bottle in a trial, not as a dry-cycle rate.
The price depends on the number of stations and heads, the mold, neck finishing, take-out and conveying, and auxiliary equipment. Compare quotations against the same container, output and scope; the cost guide lists what to include.
Let's build your next production line
Share your container, material and production requirements. We’ll help you identify a suitable machine configuration.
Discuss your project